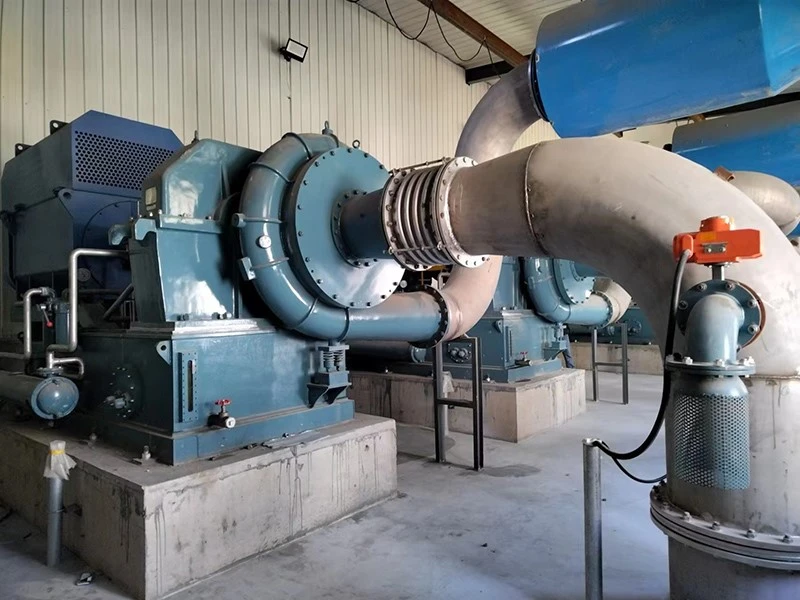
Simple Structure: The structure of a water ring vacuum pump is relatively simple, mainly composed of a pump body, impeller, and shaft, making it easy to manufacture and maintain.
Stable Operation: Due to the presence of the liquid ring, the water ring vacuum pump maintains relatively stable performance during operation and is not easily affected by changes in gas properties.
Wide Application Range: Water ring vacuum pumps can handle gases containing a certain amount of water vapor and small particles, making them suitable for various industrial applications.
Energy Saving and Environmentally Friendly: Compared to some other types of vacuum pumps, water ring vacuum pumps consume less energy during operation and generate less noise and vibration, meeting energy saving and environmental protection requirements.
Chemical Industry: Used in processes such as vacuum evaporation, vacuum drying, and vacuum filtration.
Pharmaceutical Industry: Used in vacuum drying, vacuum concentration, and vacuum distillation of pharmaceuticals.
Food Industry: Used in vacuum packaging, vacuum cooling, and vacuum dehydration of food products.
Power Industry: Used for vacuuming condensers and recovering exhaust gas from steam turbines.